
Sodium-ion battery manufacturing has moved from laboratory research to commercial production faster than many industry observers expected. Sodium is the sixth most abundant element in Earth’s crust, and its compounds are inexpensive, geographically widespread, and free from the supply-chain concentration that affects lithium, cobalt, and nickel. For equipment buyers and factory planners, the practical question is no longer whether sodium-ion cells work, but how production lines must change to make them reliably at scale. This guide covers the materials, process steps, equipment adaptations, and commercial benchmarks that define sodium-ion battery manufacturing today.
Why Sodium-Ion Battery Manufacturing Is Gaining Traction
The economics of sodium-ion battery manufacturing rest on two pillars: raw material cost and manufacturing compatibility. Sodium precursors cost substantially less than lithium precursors, and the most developed cathode families avoid cobalt and nickel entirely. Hard carbon anodes can be derived from biomass, coal tar pitch, and other carbon precursors rather than high-purity natural or synthetic graphite. Aluminum foil can serve as the current collector on both electrodes because sodium does not form an alloy with aluminum at anode operating potentials, eliminating the copper foil used in most lithium-ion anodes.
The main trade-off is energy density. Commercial sodium-ion cells typically deliver 100 to 160 Wh/kg at the cell level, while mainstream lithium-ion NMC cells deliver approximately 180 to 270 Wh/kg. This difference limits sodium-ion to applications where cost, safety, and material availability matter more than gravimetric energy: grid-scale stationary storage, backup power, two-wheelers, and low-speed electric vehicles. For these applications, lower material cost and the ability to build cells with existing production platforms can make sodium-ion battery manufacturing an attractive investment.
Materials That Define Sodium-Ion Battery Manufacturing
Cathode Families: Layered Oxides, Prussian Blue Analogues, and Polyanionic Compounds
Three cathode families dominate current development and production.
Layered oxides such as O3-type NaNi1/3Fe1/3Mn1/3O2 deliver roughly 120 to 150 mAh/g between 2.0 and 4.0 V versus Na/Na+, with an average discharge voltage near 3.0 to 3.2 V. They offer the highest practical energy density among sodium cathodes and can be produced with familiar oxide synthesis, mixing, and coating equipment. Their main weakness is moisture sensitivity: exposure to humid air forms sodium hydroxide and sodium carbonate on particle surfaces, so slurry preparation and coating must be humidity-controlled.
Prussian blue analogues such as NaxFe[Fe(CN)6] deliver approximately 120 to 160 mAh/g with excellent rate capability and very low raw material cost based on iron and cyanide precursors. Lattice water in the crystal structure must be controlled during synthesis and electrode drying because it reacts during cell operation and reduces capacity. Some Prussian blue electrode formulations can be processed with water-based slurries, which simplifies solvent handling on the line.
Polyanionic compounds, most notably Na3V2(PO4)3, operate at a flat plateau near 3.4 V with roughly 110 to 120 mAh/g and outstanding thermal stability and cycle life. The high cost and toxicity of vanadium limit their use in low-cost storage applications, but they remain relevant for products that prioritize safety and longevity.
Hard Carbon Anodes
The anode in nearly all commercial sodium-ion cells is hard carbon, a disordered carbon material with a specific capacity of approximately 250 to 350 mAh/g. Sodium ions are stored in graphitic-like domains, disordered regions, and micropores across a voltage range that includes a long plateau below roughly 0.2 V. First-cycle coulombic efficiency is typically 75 to 88 percent, lower than the 90 to 95 percent achieved with graphite anodes in lithium-ion cells, because more sodium is consumed during initial solid-electrolyte interphase formation and irreversible storage sites.
Hard carbon is processed with the same water-based CMC/SBR binder system used for graphite anodes. Precursor selection, pyrolysis temperature, and particle morphology affect reversible capacity and efficiency, which means raw material qualification is a larger part of sodium-ion battery manufacturing than chemistry selection alone.
Electrolyte and Current Collectors
Most sodium-ion electrolytes use NaPF6 dissolved in carbonate solvents such as ethylene carbonate and diethyl carbonate, with additive packages tuned for hard carbon surfaces. The electrolyte salt is hygroscopic, so moisture control around electrolyte preparation and filling remains important. Because sodium does not alloy with aluminum at low potential, aluminum foil replaces copper on the anode side. This reduces material cost, lowers cell weight, and simplifies recycling because the copper stream is removed from the cell.
Process Similarities: Reusing Lithium-Ion Equipment for Sodium-Ion Battery Manufacturing
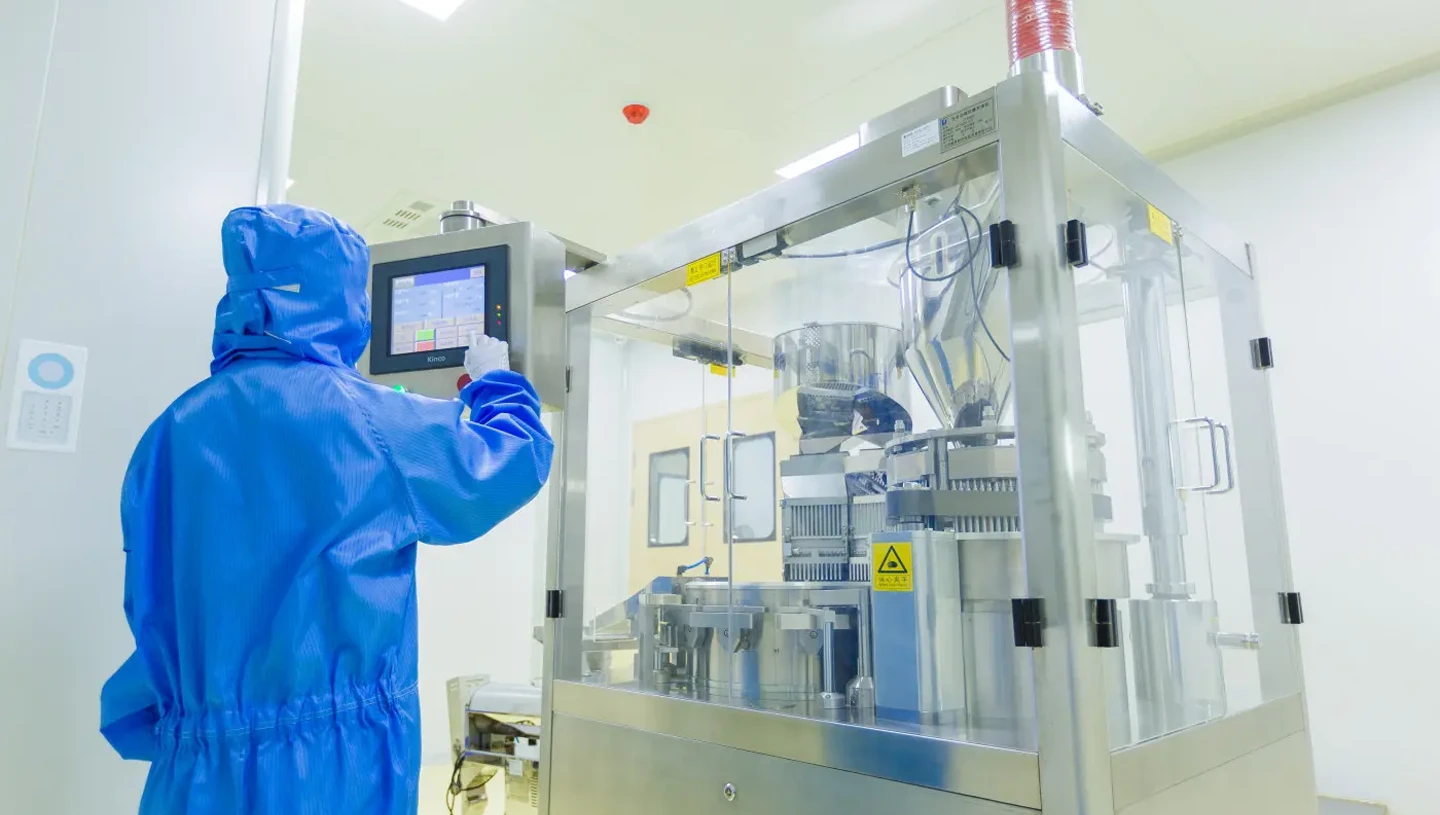
The most important commercial insight is that sodium-ion battery manufacturing shares the same overall process sequence as lithium-ion: slurry mixing, slot-die coating, drying, calendering, slitting, winding or stacking, cell assembly, tab welding, electrolyte filling, formation, aging, and end-of-line testing. A pouch, prismatic, or cylindrical line designed for lithium-ion cells can typically be converted to sodium-ion battery manufacturing with parameter changes, process optimization, and change parts rather than wholesale equipment replacement.
The degree of conversion depends on the chemistry. Water-based anode processing is already standard in lithium-ion production, so hard carbon anodes run on familiar coating and drying equipment. Cathode processing depends on the active material: layered oxides behave similarly to lithium transition-metal oxides and may retain NMP/PVDF processing, while some Prussian blue and polyanionic formulations can use alternative binder systems and drying strategies. Equipment suppliers increasingly offer mixed-chemistry lines that allow a producer to switch between lithium-ion and sodium-ion products with reduced changeover time.
Key Equipment Adaptations for Sodium-Ion Battery Manufacturing
Slurry Preparation and Coating
Hard carbon has high surface area, high pore volume, and a wide particle-size distribution compared with graphite, so slurry dispersion time, solids loading, and rheology targets must be revalidated. The coating station itself, including slot-die geometry and web handling, carries over from lithium-ion production. For moisture-sensitive cathodes, the coating environment must keep humidity low; for water-based cathode routes, solvent recovery infrastructure can be simplified or removed.
Drying and Solvent Recovery
Drying profiles must be matched to the binder system and coating thickness. Water-based anode slurries carry a higher latent heat burden than NMP-based slurries, and binder migration remains a risk when surface drying outpaces solvent transport from the coating interior. Electrode drying fundamentals apply directly to sodium-ion battery manufacturing; see the guide to battery electrode drying systems for vacuum design, temperature profiling, and residual moisture targets used in modern electrode production.
Calendering and Slitting
Hard carbon is more brittle and less compressible than graphite, so calendering pressure and roll temperature must be tuned to reach the target porosity, typically 25 to 35 percent for sodium-ion electrodes, without fracturing particles. Slitting and notching equipment is unchanged in principle, but burr limits and edge-quality inspection should be revalidated because hard carbon edges behave differently from graphite edges.
Cell Assembly and Tab Welding
Because both current collectors are aluminum, sodium-ion battery manufacturing removes the copper-aluminum dissimilar-metal joint that dominates tab-welding quality control in lithium-ion cells. Ultrasonic and laser welding parameters are set for aluminum-aluminum joints, which generally have a wider process window than aluminum-copper joints. Pouch, prismatic, and cylindrical assembly machines can be reused with format-specific change parts and revalidated weld schedules.
Electrolyte Filling and Formation
Vacuum-assisted electrolyte filling equipment carries over directly. Filling volumes and wetting times must be revalidated because hard carbon electrodes have a different pore structure and surface chemistry than graphite electrodes. Formation protocols must account for the lower first-cycle efficiency and the larger quantity of gas generated during initial SEI formation on hard carbon. Capacity grading thresholds, self-discharge limits, and aging durations are chemistry-specific and cannot simply be copied from a lithium-ion specification.
Dry Room and Quality Control
Moisture control remains critical even though sodium-ion battery manufacturing is often described as more forgiving than lithium-ion manufacturing. NaPF6 salts hydrolyze in humid air, and several cathode families degrade on exposure to water vapor. A typical cell line still controls the dry room around electrolyte handling and final assembly, with dew point targets comparable to those used for lithium-ion cells. Quality systems should add raw material qualification for hard carbon and cathode precursors, coating weight and porosity checks, weld inspection, and formation data analytics.
Current Commercialization Landscape for Sodium-Ion Battery Manufacturing
Commercial sodium-ion battery manufacturing is no longer confined to pilot plants. CATL announced its first-generation sodium-ion battery in July 2021 with a cell-level energy density of approximately 160 Wh/kg and proposed an AB pack architecture that mixes sodium-ion and lithium-ion cells to balance energy and cost CATL. Faradion, acquired by Reliance New Energy, licenses sodium-ion technology to manufacturing partners in India and other markets Faradion. Chinese producers including HiNa Battery have built hard carbon sodium-ion lines at meaningful scale, and JAC’s Yiwei brand began deliveries of sodium-ion battery electric vehicles in China in 2024.
Market analyses from organizations such as the International Energy Agency expect sodium-ion battery manufacturing to expand rapidly in stationary storage during the late 2020s, driven by battery cost pressure and the need to diversify lithium supply chains. The common thread across these developments is that commercial sodium-ion battery manufacturing relies on the same equipment ecosystem as lithium-ion, with chemistry-specific adaptation rather than a new manufacturing paradigm.
Conclusion: Is Sodium-Ion Battery Manufacturing Ready for Your Production Line?
For stationary storage, two-wheelers, and low-speed electric vehicles, the answer is yes. The materials are proven at commercial scale, the equipment platform overlaps heavily with lithium-ion production, and the raw material cost advantage is structural rather than dependent on temporary market conditions. The realistic barriers are process validation, hard carbon and cathode raw material qualification, formation yield, and the lower energy density of the final product.
Producers evaluating a conversion should audit each station against the chemistry plan: slurry solids loading and dispersion, drying temperature and residence time, calendering porosity targets, tab-welding schedules, filling wetting time, formation protocol, and quality limits. In most cases the existing line can be converted, but the conversion should be treated as a full process validation program rather than a settings change.
For producers planning new capacity, sodium-ion battery manufacturing offers a lower-cost path into the battery industry, with simpler water-based processing for hard carbon anodes and the option of aqueous cathode routes. The technology is production-ready today, and the equipment, testing, and quality frameworks built for lithium-ion provide a dependable foundation. TOBGROUP provides turnkey battery production solutions for pouch, prismatic, cylindrical, and sodium-ion chemistries, with references available in completed production line projects.


